


EN 12732:2013+A1:2014
(Main + Amendment)Gas infrastructure - Welding steel pipework - Functional requirements
General Information
- Abstract
This document amends prEN 12732 Clause 4.5 "Testing companies and personnel".
- Status
- Withdrawn
- Publication Date
- 22-Apr-2014
- Withdrawal Date
- 22-Sep-2026
- Technical Committee
- CEN/TC 234 - Gas infrastructure
- Drafting Committee
- CEN/TC 234/WG 3 - Gas Transportation
- Current Stage
- 9960 - Withdrawal effective - Withdrawal
- Start Date
- 17-Nov-2021
- Completion Date
- 23-Sep-2026


Relations
- Effective Date
- 18-Jan-2023
- Merged From
EN 12732:2013/FprA1 - Gas infrastructure - Welding steel pipework - Functional requirements - Effective Date
- 15-Jan-2014
- Effective Date
- 08-Jun-2022
- Effective Date
- 27-May-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
Get Certified
Connect with accredited certification bodies for this standard

DVS-ZERT GmbH
German welding certification society.
CARES (UK Certification Authority for Reinforcing Steels)
UK certification for reinforcing steels and construction.
EWF/IIW (European/International Welding Federation)
International welding personnel certification.
Sponsored listings
Frequently Asked Questions
EN 12732:2013+A1:2014 is a standard published by the European Committee for Standardization (CEN). Its full title is "Gas infrastructure - Welding steel pipework - Functional requirements". This standard covers: This document amends prEN 12732 Clause 4.5 "Testing companies and personnel".
This document amends prEN 12732 Clause 4.5 "Testing companies and personnel".
EN 12732:2013+A1:2014 is classified under the following ICS (International Classification for Standards) categories: 25.160.40 - Welded joints and welds. The ICS classification helps identify the subject area and facilitates finding related standards.
EN 12732:2013+A1:2014 has the following relationships with other standards: It is inter standard links to EN 12732:2013, EN 12732:2013/FprA1, EN 12732:2021, EN ISO 18275:2026, EN ISO 17632:2015, EN ISO 6520-1:2007, EN ISO 3452-4:1998, EN ISO 15611:2024, EN ISO 17637:2016, EN ISO/IEC 17020:2012, EN ISO 9606-1:2017, EN ISO 14341:2020, EN ISO 3834-1:2021, EN ISO 9692-1:2013, EN ISO 10863:2011. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
EN 12732:2013+A1:2014 is associated with the following European legislation: Standardization Mandates: M/017. When a standard is cited in the Official Journal of the European Union, products manufactured in conformity with it benefit from a presumption of conformity with the essential requirements of the corresponding EU directive or regulation.
EN 12732:2013+A1:2014 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.Gasinfrastruktur - Schweißen an Rohrleitungen aus Stahl - Funktionale AnforderungenInfrastructures gazières - Soudage des tuyauteries en acier - Prescriptions fonctionnellesGas infrastructure - Welding steel pipework - Functional requirements91.140.40Sistemi za oskrbo s plinomGas supply systems25.160.40Varjeni spoji in variWelded jointsICS:Ta slovenski standard je istoveten z:EN 12732:2013+A1:2014SIST EN 12732:2013+A1:2014en,fr,de01-junij-2014SIST EN 12732:2013+A1:2014SLOVENSKI
STANDARDSIST EN 12732:20131DGRPHãþD
EUROPEAN STANDARD NORME EUROPÉENNE EUROPÄISCHE NORM
EN 12732:2013+A1
April 2014 ICS 25.160.40 Supersedes EN 12732:2013English Version
Gas infrastructure - Welding steel pipework - Functional requirements
Infrastructures gazières - Soudage des tuyauteries en acier - Prescriptions fonctionnelles
Gasinfrastruktur - Schweißen an Rohrleitungen aus Stahl - Funktionale Anforderungen This European Standard was approved by CEN on 14 March 2013 and includes Amendment 1 approved by CEN on 3 February 2014.
CEN members are bound to comply with the CEN/CENELEC Internal Regulations which stipulate the conditions for giving this European Standard the status of a national standard without any alteration. Up-to-date lists and bibliographical references concerning such national standards may be obtained on application to the CEN-CENELEC Management Centre or to any CEN member.
This European Standard exists in three official versions (English, French, German). A version in any other language made by translation under the responsibility of a CEN member into its own language and notified to the CEN-CENELEC Management Centre has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia, Finland, Former Yugoslav Republic of Macedonia, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Romania, Slovakia, Slovenia, Spain, Sweden, Switzerland, Turkey and United Kingdom.
EUROPEAN COMMITTEE FOR STANDARDIZATION
COMITÉ EUROPÉEN DE NORMALISATION EUROPÄISCHES KOMITEE FÜR NORMUNG
CEN-CENELEC Management Centre:
Avenue Marnix 17,
B-1000 Brussels © 2014 CEN All rights of exploitation in any form and by any means reserved worldwide for CEN national Members. Ref. No. EN 12732:2013+A1:2014 ESIST EN 12732:2013+A1:2014
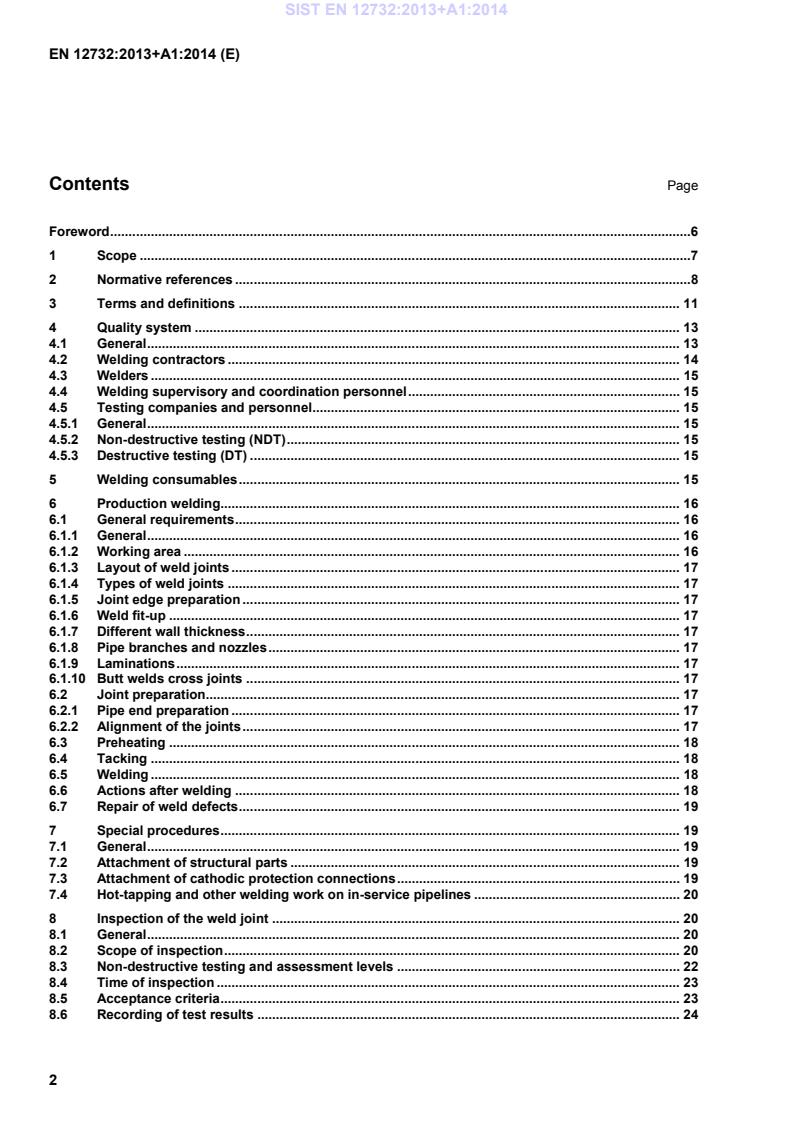
Contents Page Foreword .6 1 Scope .7 2 Normative references .8 3 Terms and definitions . 11 4 Quality system . 13 4.1 General . 13 4.2 Welding contractors . 14 4.3 Welders . 15 4.4 Welding supervisory and coordination personnel . 15 4.5 Testing companies and personnel . 15 4.5.1 General . 15 4.5.2 Non-destructive testing (NDT) . 15 4.5.3 Destructive testing (DT) . 15 5 Welding consumables . 15 6 Production welding. 16 6.1 General requirements . 16 6.1.1 General . 16 6.1.2 Working area . 16 6.1.3 Layout of weld joints . 17 6.1.4 Types of weld joints . 17 6.1.5 Joint edge preparation . 17 6.1.6 Weld fit-up . 17 6.1.7 Different wall thickness . 17 6.1.8 Pipe branches and nozzles . 17 6.1.9 Laminations . 17 6.1.10 Butt welds cross joints . 17 6.2 Joint preparation. 17 6.2.1 Pipe end preparation . 17 6.2.2 Alignment of the joints . 17 6.3 Preheating . 18 6.4 Tacking . 18 6.5 Welding . 18 6.6 Actions after welding . 18 6.7 Repair of weld defects . 19 7 Special procedures . 19 7.1 General . 19 7.2 Attachment of structural parts . 19 7.3 Attachment of cathodic protection connections . 19 7.4 Hot-tapping and other welding work on in-service pipelines . 20 8 Inspection of the weld joint . 20 8.1 General . 20 8.2 Scope of inspection . 20 8.3 Non-destructive testing and assessment levels . 22 8.4 Time of inspection . 23 8.5 Acceptance criteria . 23 8.6 Recording of test results . 24 SIST EN 12732:2013+A1:2014
9 Documentation . 24 9.1 General . 24 9.2 Archiving requirements . 24 10 Specific requirements for gas infrastructure with a MOP up to and including 16 bar . 24 10.1 General . 24 10.2 Welders . 24 10.3 Welding supervisory personnel . 25 10.4 Production welding . 25 10.4.1 General . 25 10.4.2 Joint preparation . 25 10.4.3 Welding . 25 10.5 Requirements for records and documentation . 25 11 Specific requirements for gas infrastructure with a MOP greater than 16 bar . 26 11.1 General . 26 11.2 Welders . 26 11.3 Welding supervisory personnel . 26 11.4 Qualification of welding procedures . 26 11.4.1 General . 26 11.4.2 Filler material requirements for welding procedure qualification . 26 11.4.3 Impact testing . 27 11.4.4 Transverse tensile test . 27 11.4.5 All-weld-metal tensile test . 28 11.5 Production welding . 28 11.5.1 General . 28 11.5.2 Joint preparation . 28 11.5.3 Welding . 28 11.5.4 Repairs of weld defects . 29 11.5.5 Welding consumables . 29 11.6 Destructive testing of production welds . 29 11.7 Acceptance requirements. 29 11.8 Requirements for records and documentation . 30 12 Specific requirements for metering, regulating and compressor stations . 31 12.1 General . 31 12.2 Specific requirements . 31 Annex A (informative)
Qualification procedure for pipeline welders (Girth welds and branch connections) . 32 A.1 General . 32 A.2 Approval test . 32 A.2.1 Execution of the approval test . 32 A.2.2 Range of test pieces . 32 A.2.3 Supervision of execution of approval test . 33 A.3 Inspection . 33 A.3.1 General . 33 A.3.2 Testing girth welds . 34 A.3.3 Testing weldolets . 34 A.4 Approval range . 34 A.4.1 General . 34 A.4.2 Dimension ranges . 34 SIST EN 12732:2013+A1:2014
A.4.3 Techniques . 34 A.5 Certificate . 35 A.5.1 General . 35 A.5.2 Duration of validity . 35 Annex B (informative)
Testing of lamination defects . 36 Annex C (informative)
Time-of-flight diffraction technique (TOFD) . 37 C.1 General . 37 C.2 Additional and substitutional requirements to EN ISO 10863:2011 . 37 C.2.1 Addition to the whole document EN ISO 10863:2011 . 37 C.2.2 Addition to EN ISO 10863:2011, Clause 3 "Terms and definitions" . 37 C.2.3 Addition to EN ISO 10863:2011, Clause 5, "Examination Levels" . 39 C.2.4 Addition to EN ISO 10863:2011, 7.2.2, "Ultrasonic probes" . 39 C.2.5 Substitution of EN ISO 10863:2011, Clause 11, 3rd paragraph "Weld testing" . 39 C.2.6 Substitution of EN ISO 10863:2011, 12.5.2 "Sizing" . 40 Annex D (informative)
Critical aspects for hot-tap welding or welding on in-service pipelines . 45 D.1 General . 45 D.2 Recommendations . 45 D.2.1 Equipment . 45 D.2.2 Supervision . 45 D.2.3 Safety precautions . 45 D.2.4 Identification . 45 D.2.5 Filler materials . 45 D.3 Weld preparation. 46 D.4 Welding procedure specification (WPS) . 46 D.4.1 Description of the WPS . 46 D.4.2 Qualification of the WPS . 46 D.4.3 Approval of the WPS . 46 D.5 Qualification of the welder . 46 D.6 Precautions . 46 D.7 Execution . 47 D.8 Repairs . 47 D.9 WPS qualification record . 47 Annex E (informative)
Visual examination of joints . 49 E.1 General . 49 E.2 Recommendations . 49 Annex F (informative)
Manual ultrasonic testing of weld joints for wall thickness between approximately 6 mm and 8 mm . 50 F.1 General . 50 SIST EN 12732:2013+A1:2014
F.2 Setting . 50 F.2.1 Setting of range . 50 F.2.2 Sensitivity adjustment when using the Distance Gain Size method . 50 Annex G (normative)
Acceptance criteria - Recommendations for on-site production welds . 54 G.1 General . 54 G.2 Acceptance criteria according to EN ISO 5817 . 54 G.3 Summary of requirements for defect acceptance levels and defect limits . 57 G.3.1 General . 57 G.3.2 Requirements . 58 G.4 Method and acceptance criteria for ultrasonic inspection assessment . 65 G.4.1 Distance Gain Size method . 65 G.4.2 Comparative Element method . 65 G.4.3 General . 65 G.4.4 Assessment of indications using automatic pulse-echo technique . 67 Annex H (informative)
Brazing and aluminothermic welding of leads for cathodic protection systems . 68 H.1 Joining techniques . 68 H.2 Procedure qualification . 68 H.3 Operation qualification . 70 H.4 Production joints . 70 Annex I (informative)
Significant technical changes between this European Standard and the previous edition . 71 Bibliography . 72
Foreword This document (EN 12732:2013+A1:2014) has been prepared by Technical Committee CEN/TC 234 “Gas infrastructure”, the secretariat of which is held by DIN. This European Standard shall be given the status of a national standard, either by publication of an identical text or by endorsement, at the latest by October 2014, and conflicting national standards shall be withdrawn at the latest by October 2014. Attention is drawn to the possibility that some of the elements of this document may be the subject of patent rights. CEN [and/or CENELEC] shall not be held responsible for identifying any or all such patent rights. This document supersedes !EN 12732:2013". This document includes Amendment 1 approved by CEN on 2014-02-03. The start and finish of text introduced or altered by amendment is indicated in the text by tags !". This European Standard has been prepared under mandate M/017 given to CEN by the Commission of the European Communities and the European Free Trade Association. Annex I provides details of significant technical changes between this European Standard and the previous edition. There is a complete suite of functional standards prepared by CEN/TC 234 ”Gas infrastructure“ to cover all parts from the input of gas to the transmission system up to the inlet connection of the gas appliances, whether for domestic, commercial or industrial purposes. In preparing this standard a basic understanding of gas infrastructure by the user has been assumed. Gas infrastructure is complex and the importance on safety of its construction and use has led to the development of very detailed codes of practice and operating manuals in the member countries. These detailed statements embrace recognised standards of gas engineering and the specific requirements imposed by the legal structures of the member countries. CEN/TC 234 will continue its work updating this standard to the latest developments at regular intervals. According to the CEN-CENELEC Internal Regulations, the national standards organizations of the following countries are bound to implement this European Standard: Austria, Belgium, Bulgaria, Croatia, Cyprus, Czech Republic, Denmark, Estonia, Finland, Former Yugoslav Republic of Macedonia, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Romania, Slovakia, Slovenia, Spain, Sweden, Switzerland, Turkey and the United Kingdom.
1 Scope This European Standard contains requirements for the production and testing of weld joints for the installation and modification of onshore steel pipelines and pipework used in gas infrastructure, including in-service pipelines, for all pressure ranges for the carriage of processed, non-toxic and non-corrosive natural gas according to EN ISO 13686 and for the carriage of non-conventional gases such as injected biomethane, where — the pipeline elements are made of unalloyed or low-alloyed carbon steel; — the pipeline is not located within commercial or industrial premises as integral part of the industrial process on those premises except for any pipelines and facilities delivering gas to such premises; — the pipework is not located within household installations according to EN 1775; — the design temperature of the system is between -40 °C up to and including 120 °C. The onshore steel pipelines and pipework used in gas infrastructure include in-service pipelines, for all pressure ranges for the carriage of processed, non-toxic and non-corrosive natural gas according to EN ISO 13686 and for the carriage of non-conventional gases complying with EN ISO 13686, and for which a detailed technical evaluation of the functional requirements (such as injected biomethane) is performed ensuring there are no other constituents or properties of the gases that can affect the integrity of the pipeline. This standard is not applicable to welds produced prior to the publication of this European Standard. Table 1 assigns the application areas to quality requirement categories as a function of the working pressure and pipe materials used. Table 1 — Allocation to quality requirement categories Quality requirement category Area of activity applies to B Pressure range and base material
≤ 5 b~r Group 1.1, 1.2 and 1.4 according to CEN ISO/TR 15608 Rt 0,5 ≤ 360 k/mm2 Examples of use: Mains and service pipes in gas distribution systems, pipework in stations C Pressure range and base material
> 5 b~r ≤ k6 b~r Group 1.1, 1.2 and 1.4 according to CEN ISO/TR 15608 Rt 0,5 ≤ 360 k/mm2 Examples of use: Pipelines including pipework in stations and gas distribution systems D Pressure range or base material
> 16 bar a Group 1, 2 and 3 according to CEN ISO/TR 15608 SIST EN 12732:2013+A1:2014
Quality requirement category Area of activity applies to Examples of use: Pipelines including pipework in stations and gas transmission systems Key Rt 0,5 is the specified minimum yield strength according to EN ISO 3183. NOTE 1 "Category A" for pipework up to and including 100 mbar, as mentioned in the previous version EN 12732:2000, has been incorporated in the pressure range of "Category B" and has been deleted from this table. NOTE 2 Gas infrastructure with a MOP up to and including 16 bar is generally dedicated to gas distribution. a Pipelines having hoop stresses at design pressure up to 30 % of specified minimum yield strength (Rt 0,5) and operated at a pressure up to 24 bar may be allocated to quality requirement Category C by the pipeline operator. Additional requirements may be specified when, for example: — the strain on pipelines and systems, — the materials, — the line routing, — the design or the welding technique are considered critical. This European Standard specifies common basic principles for gas infrastructure. Users of this European Standard should be aware that there can exist more detailed national standards and/or codes of practice in the CEN member countries. This European Standard is intended to be applied in association with these national standards and/or codes of practice setting out the above-mentioned basic principles. In the event of conflicts in terms of more restrictive requirements in national legislation/regulation with the requirements of this standard, the national legislation/regulation takes precedence as illustrated in CEN/TR 13737 (all parts). NOTE CEN/TR 13737 (all parts) contains: — clarification of relevant legislation/regulations applicable in a country; — if appropriate, more restrictive national requirements; — national contact point for the latest information. 2 Normative references The following documents, in whole or in part, are normatively referenced in this document and are indispensable for its application. For dated references, only the edition cited applies. For undated references, the latest edition of the referenced document (including any amendments) applies. SIST EN 12732:2013+A1:2014
EN 287-1, Qualification test of welders — Fusion welding — Part 1: Steels EN 1418:1997, Welding personnel — Approval testing of welding operators for fusion welding and resistance weld setters for fully mechanized and automatic welding of metallic materials EN 1708-1, Welding - Basic welded joint details in steel - Part 1: Pressurized components EN 10204, Metallic products - Types of inspection documents EN ISO 636, Welding consumables — Rods, wires and deposits for tungsten inert gas welding of non-alloy and fine-grain steels — Classification (ISO 636) EN ISO 2560, Welding consumables — Covered electrodes for manual metal arc welding of non-alloy and fine grain steels — Classification (ISO 2560) EN ISO 3183, Petroleum and natural gas industries — Steel pipe for pipeline transportation systems (ISO 3183) EN ISO 3452 (all parts), Non-destructive testing — Penetrant testing (ISO 3452) EN ISO 3834-1, Quality requirements for fusion welding of metallic materials — Part 1: Criteria for the selection of the appropriate level of quality requirements (ISO 3834-1) EN ISO 3834-2, Quality requirements for fusion welding of metallic materials — Part 2: Comprehensive quality requirements (ISO 3834-2) EN ISO 3834-3, Quality requirements for fusion welding of metallic materials — Part 3: Standard quality requirements (ISO 3834-3) EN ISO 3834-4, Quality requirements for fusion welding of metallic materials — Part 4: Elementary quality requirements (ISO 3834-4) EN ISO 5817, Welding — Fusion-welded joints in steel, nickel, titanium and their alloys (beam welding excluded) — Quality levels for imperfections (ISO 5817) EN ISO 6520-1, Welding and allied processes — Classification of geometric imperfections in metallic materials — Part 1: Fusion welding (ISO 6520-1) EN ISO 6892-1, Metallic materials — Tensile testing — Part 1: Method of test at room temperature (ISO 6892-1) EN ISO 9692-1, Welding and allied processes — Recommendations for joint preparation — Part 1: Manual metal-arc welding, gas-shielded metal-arc welding, gas welding, TIG welding and beam welding of steels (ISO 9692-1) EN ISO 9712, Non-destructive testing — Qualification and certification of NDT personnel (ISO 9712) EN ISO 10863:2011, Non-destructive testing of welds - Ultrasonic testing - Use of time-of-flight diffraction technique (TOFD) (ISO 10863:2011) EN ISO 14171, Welding consumables — Solid wire electrodes, tubular cored electrodes and electrode/flux combinations for submerged arc welding of non alloy and fine grain steels — Classification (ISO 14171) EN ISO 14174, Welding consumables — Fluxes for submerged arc welding and electroslag welding — Classification (ISO 14174) SIST EN 12732:2013+A1:2014
EN ISO 14175, Welding consumables — Gases and gas mixtures for fusion welding and allied processes (ISO 14175) EN ISO 14341, Welding consumables — Wire electrodes and weld deposits for gas shielded metal arc welding of non alloy and fine grain steels - Classification (ISO 14341) EN ISO 14731, Welding coordination — Tasks and responsibilities (ISO 14731) EN ISO 15607:2003, Specification and qualification of welding procedures for metallic materials - General rules (ISO 15607:2003) CEN ISO/TR 15608, Welding — Guidelines for a metallic materials grouping system (ISO/TR 15608) EN ISO 15609-1, Specification and qualification of welding procedures for metallic materials — Welding procedure specification — Part 1: Arc welding (ISO 15609-1) EN ISO 15609-2, Specification and qualification of welding procedures for metallic materials — Welding procedure specification — Part 2: Gas welding (ISO 15609-2) EN ISO 15610, Specification and qualification of welding procedures for metallic materials — Qualification based on tested welding consumables (ISO 15610) EN ISO 15611, Specification and qualification of welding procedures for metallic materials — Qualification based on previous welding experience (ISO 15611) EN ISO 15612, Specification and qualification of welding procedures for metallic materials — Qualification by adoption of a standard welding procedure (ISO 15612) EN ISO 15613, Specification and qualification of welding procedures for metallic materials — Qualification based on pre-production welding test (ISO 15613) EN ISO 15614-1, Specification and qualification of welding procedures for metallic materials — Welding procedure test — Part 1: Arc and gas welding of steels and arc welding of nickel and nickel alloys (ISO 15614-1) EN ISO/IEC 17020, Conformity assessment — Requirements for the operation of various types of bodies performing inspection (ISO/IEC 17020) EN ISO/IEC 17025, General requirements for the competence of testing and calibration laboratories (ISO/IEC 17025) EN ISO 17636-1, Non-destructive testing of welds — Radiographic testing — Part 1: X- and gamma-ray techniques with film (ISO 17636-1) EN ISO 17636-2, Non-destructive testing of welds — Radiographic testing — Part 2: X- and gamma-ray techniques with digital detectors (ISO 17636-2) EN ISO 17632, Welding consumables — Tubular cored electrodes for gas shielded and non-gas shielded metal arc welding of non-alloy and fine grain steels — Classification (ISO 17632) EN ISO 17637, Non-destructive testing of welds — Visual testing of fusion-welded joints (ISO 17637) EN ISO 17638, Non-destructive testing of welds — Magnetic particle testing (ISO 17638) EN ISO 17640, Non-destructive testing of welds — Ultrasonic testing — Techniques, testing levels, and assessment (ISO 17640) SIST EN 12732:2013+A1:2014
EN ISO 18275, Welding consumables — Covered electrodes for manual metal arc welding of high-strength steels — Classification (ISO 18275) IIW-IAB -252-07, Personnel with responsibility for welding coordination 3 Terms and definitions For the purposes of this document, the following terms and definitions apply. Symbols used in formulae are defined where they occur. 3.1 design temperature DT temperature on which the design calculations are based 3.2 gas gaseous fuel which is in a gaseous state at a temperature of 15 °C under atmospheric pressure (1,013 25 bar absolute) 3.3 gas infrastructure all pipelines, stations and installations from the input of gas to the transmission system up to the inlet connection of the gas appliances, whether for domestic, commercial or industrial purposes 3.4 gas distribution system pipeline system including piping above and below ground and all other equipment necessary to deliver the gas to the consumer 3.5 gas transmission activity intended to convey gas from one place to another through pipelines in order to deliver gas to distribution systems or to industrial consumers 3.6 installation equipment and facilities for the extraction, production, chemical treatment, measurement, control, storage or off-take of the transported gas 3.7 maximum operating pressure MOP maximum pressure at which a system can be operated continuously under normal conditions Note 1 to entry: normal conditions are: no fault in any device or stream 3.8 national requirements requirements following from national legislation or more detailed or stringent national standards 3.9 onshore pipeline buried and/or above ground pipeline including those sections laid in or across inland lakes or water courses SIST EN 12732:2013+A1:2014
3.10 pipeline system of pipework with all associated equipment and stations up to the point of delivery. This pipework is mainly below ground but also includes above ground parts 3.11 pipeline components elements from which a pipeline is constructed. The following are distinct pipeline elements: — pipe including cold-formed bends; — fittings EXAMPLE 1 Reducers, tees, factory-made elbows and bends, flanges, caps, welding stubs, mechanical joints — fabrications, manufactured from elements referred above; EXAMPLE 2 Manifolds, slug catchers, pig launching/receiving stations, metering and control runs — equipment EXAMPLE 3 Valves, expansion joints, insulating joints, pressure regulators, pumps, compressors — pressure vessels 3.12 pipeline operator private or public organisation authorised to design, construct, and/or operate and maintain the gas infrastructure, i.e. gas transmission operators (TSO) and gas distribution operators (DSO) 3.13 pipework assembly of pipes and fittings 3.14 pressure gauge pressure of the fluid inside the system, measured in static conditions 3.15 station plant or facility for the operation and/or processing of gas infrastructure 3.16 test pressure TP pressure to which a part of the gas infrastructure is subjected to, to ensure safe operation Note 1 to entry: The test pressure can be different for the different parts of the infrastructure to be tested. 3.17 weld repair process of repairing a defect that is discovered after the weld has been completed, by additional welding and submitted for inspection Note 1 to entry: The repair can involve complete removal of a cylinder of pipe or removal of a localised area by grinding or other means followed by additional welding. SIST EN 12732:2013+A1:2014
3.18 welder person who holds and manipulates the electrode holder, welding torch or blow pipe by hand 3.19 welding procedure specification (WPS) a document that has been qualified by one of the methods described in EN ISO 15607:2003, Clause 6, and provides the required variables of the welding procedure to ensure repeatability during production welding 3.20 temper bead method a weld sequence whereby the heat-affected zone of the base material is softened as much as possible 3.21 Hydrogen Dissolved in Metal HDM the amount of diffusible hydrogen in 100 mg of weld metal 4 Quality system 4.1 General If required by the pipeline operator, a quality system shall be applied to pipeline welding. A set of recommended quality requirements according to EN ISO 3834 is provided in Table 2, which specifies the requirements of EN ISO 3834 for the different categories as defined in Table 1. SIST EN 12732:2013+A1:2014
Table 2 — Recommended quality requirements Requirement relating to: Quality requirement category in accordance with Table 1 B C D Quality system according to:
— EN ISO 3834-1 and EN ISO 3834-2 (complete) + ≤ ≤ — EN ISO 3834-1 and EN ISO 3834-3 (standard) + ≤ ≤ — EN ISO 3834-1 and EN ISO 3834-4 (elementary) ≤ - - Welding coordination personnel:
— Personnel according to EN ISO 14731:
— welding engineer + + ≤ — welding technologist + ≤ - a — welding specialist ≤ ≤ - a — Welding practitioner as defined in IIW-IAB-252-07 ≤ - - — Testing personnel according to EN ISO 9712 ≤ ≤ ≤ Welding procedure specification (WPS):
— According to EN ISO 15609-1 ≤ ≤ ≤ — According to EN ISO 15609-2 (up to 100 mbar) ≤ - - Approval of welding procedures according to one of the following standards:
— EN ISO 15614-1 (welding procedure test) + ≤ ≤ — EN ISO 15610 (using approved welding consumables) ≤ - - — EN ISO 15611 (previous experience) - - - — EN ISO 15612 (standard welding procedures)a + ≤ ≤ — EN ISO 15613 (pre-production welding test) ≤ ≤ ≤ Key ≤ recommended + optional - not recommended a This may also be applicable in Category D for small projects or for materials with Rt 0,5 ≤ 360 k/mm². 4.2 Welding contractors If required by the pipeline operator, contractors shall demonstrate their ability to perform the work. Reference can be made to EN ISO 3834. SIST EN 12732:2013+A1:2014
4.3 Welders All welders shall be qualified for the work they are required to undertake. The qualification should be carried out in accordance with Clauses 10, 11 and 12. 4.4 Welding supervisory and coordination personnel If a quality system is required by the pipeline operator, the supervisory and the coordination personnel should be qualified according to EN ISO 14731 as indicated in Table 2. Welding tasks and responsibilities for welding shall be clearly assigned to personnel with the appropriate experience and technical knowledge. 4.5 Testing companies and personnel 4.5.1 General Destructive testing and non-destructive testing personnel shall be employed either by the pipeline contractor or by
...