


EN 10326:2004
(Main)Continuously hot-dip coated strip and sheet of structural steels - Technical delivery conditions
General Information
- Abstract
1.1 This European Standard specifies requirements for continuously hot-dip coated products made of structural steels coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), aluminium-zinc alloy (AZ) and aluminium-silicon alloy (AS) (see Table 1) with thicknesses from 0,35 mm up to 3,0 mm unless otherwise agreed (see 1.2). The thickness is the final thickness of the delivered product after coating.
This European Standard applies to strip of all widths and to sheets cut from it (= 600 mm width) and cut lengths
(< 600 mm width).
1.2 If agreed at the time of enquiry and order, this European Standard may also be applied to continuously hot-dip coated flat products in thicknesses > 3,0 mm. In this case the mechanical property, adhesion of coating and surface condition requirements shall also be agreed at the time of enquiry and order.
1.3 The products covered by this European Standard are mainly used where minimum yield strength and corrosion resistance are the most important factors. Corrosion resistance of the alloy is proportional to the coating thickness, hence to its mass (see also 7.3.2).
NOTE +ZF coated products should not be used without additional organic coating.
1.4 This European Standard is not applicable to:
· continuously hot-dip coated flat products of low-carbon steel strip and sheet for cold forming (see prEN 10327);
· electrolytic galvanized cold rolled steel flat products (see EN 10152);
· continuously organic coated (coil coated) flat steel products (see EN 10169-1, ENV 10169-2 and
EN 10169-3);
· continuously hot-dip coated strip and sheet of steels with higher yield strength for cold forming (see EN 10292).
- Status
- Withdrawn
- Publication Date
- 06-Jul-2004
- Withdrawal Date
- 10-Mar-2009
- Technical Committee
- ECISS/TC 109 - Coated and uncoated flat products to be used for cold forming
- Current Stage
- 9960 - Withdrawal effective - Withdrawal
- Start Date
- 11-Mar-2009
- Completion Date
- 11-Mar-2009

Relations
- Effective Date
- 22-Dec-2008
- Effective Date
- 22-Dec-2008
- Effective Date
- 22-Dec-2008
- Effective Date
- 22-Dec-2008
- Replaced By
EN 10346:2009 - Continuously hot-dip coated steel flat products - Technical delivery conditions - Effective Date
- 23-Mar-2009
- Effective Date
- 28-Jan-2026
- Effective Date
- 28-Jan-2026
Get Certified
Connect with accredited certification bodies for this standard
Element Materials Technology
Materials testing and product certification.

Inštitut za kovinske materiale in tehnologije
Institute of Metals and Technology. Materials testing, metallurgical analysis, NDT.
Sponsored listings
Frequently Asked Questions
EN 10326:2004 is a standard published by the European Committee for Standardization (CEN). Its full title is "Continuously hot-dip coated strip and sheet of structural steels - Technical delivery conditions". This standard covers: 1.1 This European Standard specifies requirements for continuously hot-dip coated products made of structural steels coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), aluminium-zinc alloy (AZ) and aluminium-silicon alloy (AS) (see Table 1) with thicknesses from 0,35 mm up to 3,0 mm unless otherwise agreed (see 1.2). The thickness is the final thickness of the delivered product after coating. This European Standard applies to strip of all widths and to sheets cut from it (= 600 mm width) and cut lengths (< 600 mm width). 1.2 If agreed at the time of enquiry and order, this European Standard may also be applied to continuously hot-dip coated flat products in thicknesses > 3,0 mm. In this case the mechanical property, adhesion of coating and surface condition requirements shall also be agreed at the time of enquiry and order. 1.3 The products covered by this European Standard are mainly used where minimum yield strength and corrosion resistance are the most important factors. Corrosion resistance of the alloy is proportional to the coating thickness, hence to its mass (see also 7.3.2). NOTE +ZF coated products should not be used without additional organic coating. 1.4 This European Standard is not applicable to: · continuously hot-dip coated flat products of low-carbon steel strip and sheet for cold forming (see prEN 10327); · electrolytic galvanized cold rolled steel flat products (see EN 10152); · continuously organic coated (coil coated) flat steel products (see EN 10169-1, ENV 10169-2 and EN 10169-3); · continuously hot-dip coated strip and sheet of steels with higher yield strength for cold forming (see EN 10292).
1.1 This European Standard specifies requirements for continuously hot-dip coated products made of structural steels coated with zinc (Z), zinc-iron alloy (ZF), zinc-aluminium alloy (ZA), aluminium-zinc alloy (AZ) and aluminium-silicon alloy (AS) (see Table 1) with thicknesses from 0,35 mm up to 3,0 mm unless otherwise agreed (see 1.2). The thickness is the final thickness of the delivered product after coating. This European Standard applies to strip of all widths and to sheets cut from it (= 600 mm width) and cut lengths (< 600 mm width). 1.2 If agreed at the time of enquiry and order, this European Standard may also be applied to continuously hot-dip coated flat products in thicknesses > 3,0 mm. In this case the mechanical property, adhesion of coating and surface condition requirements shall also be agreed at the time of enquiry and order. 1.3 The products covered by this European Standard are mainly used where minimum yield strength and corrosion resistance are the most important factors. Corrosion resistance of the alloy is proportional to the coating thickness, hence to its mass (see also 7.3.2). NOTE +ZF coated products should not be used without additional organic coating. 1.4 This European Standard is not applicable to: · continuously hot-dip coated flat products of low-carbon steel strip and sheet for cold forming (see prEN 10327); · electrolytic galvanized cold rolled steel flat products (see EN 10152); · continuously organic coated (coil coated) flat steel products (see EN 10169-1, ENV 10169-2 and EN 10169-3); · continuously hot-dip coated strip and sheet of steels with higher yield strength for cold forming (see EN 10292).
EN 10326:2004 is classified under the following ICS (International Classification for Standards) categories: 77.140.10 - Heat-treatable steels; 77.140.50 - Flat steel products and semi-products. The ICS classification helps identify the subject area and facilitates finding related standards.
EN 10326:2004 has the following relationships with other standards: It is inter standard links to EN 10215:1995, EN 10154:2002, EN 10214:1995, EN 10147:2000, EN 10346:2009, EN 1994-2:2005, EN 1994-1-1:2004. Understanding these relationships helps ensure you are using the most current and applicable version of the standard.
EN 10326:2004 is available in PDF format for immediate download after purchase. The document can be added to your cart and obtained through the secure checkout process. Digital delivery ensures instant access to the complete standard document.
Standards Content (Sample)
2003-01.Slovenski inštitut za standardizacijo. Razmnoževanje celote ali delov tega standarda ni dovoljeno.Continuously hot-dip coated strip and sheet of structural steels - Technical delivery conditionsBandes et tôles en aciers de construction doux revetues en continu par immersion a chaud - Conditions techniques de livraisonKontinuierlich schmelztauchveredeltes Band und Blech aus Baustählen - Technische Lieferbedingungen77.140.50SROL]GHONLFlat steel products and semi-products77.140.10Jekla za toplotno obdelavoHeat-treatable steelsICS:SIST EN 10326:2004enTa slovenski standard je istoveten z:EN 10326:200401-november-2004SIST EN 10326:2004SLOVENSKI
STANDARDSIST EN 10214:1997SIST EN 10215:1998SIST EN 10147:2001SIST EN 10154:20031DGRPHãþD
EUROPEAN STANDARD NORME EUROPÉENNE EUROPÄISCHE NORM
EN 10326
July 2004 ICS 77.140.50; 77.140.10 Supersedes EN 10147:2000,EN 10154:2002,EN 10214:1995,and EN 10215:1995English version
Continuously hot-dip coated strip and sheet of structural steels -Technical delivery conditions
Bandes et tôles en aciers de construction doux revêtues en continu par immersion à chaud - Conditions techniques de livraison
Kontinuierlich schmelztauchveredeltes Band und Blech aus Baustählen - Technische Lieferbedingungen This European Standard was approved by CEN on 23 April 2004.
CEN members are bound to comply with the CEN/CENELEC Internal Regulations which stipulate the conditions for giving this European Standard the status of a national standard without any alteration. Up-to-date lists and bibliographical references concerning such national standards may be obtained on application to the Central Secretariat or to any CEN member.
This European Standard exists in three official versions (English, French, German). A version in any other language made by translation under the responsibility of a CEN member into its own language and notified to the Central Secretariat has the same status as the official versions.
CEN members are the national standards bodies of Austria, Belgium, Cyprus, Czech Republic, Denmark, Estonia, Finland, France, Germany, Greece, Hungary, Iceland, Ireland, Italy, Latvia, Lithuania, Luxembourg, Malta, Netherlands, Norway, Poland, Portugal, Slovakia, Slovenia, Spain, Sweden, Switzerland and United Kingdom.
EUROPEAN COMMITTEE FOR STANDARDIZATION COMITÉ EUROPÉEN DE NORMALISATION EUROPÄISCHES KOMITEE FÜR NORMUNG
Management Centre: rue de Stassart, 36
B-1050 Brussels © 2004 CEN All rights of exploitation in any form and by any means reserved worldwide for CEN national Members. Ref. No. EN 10326:2004: E
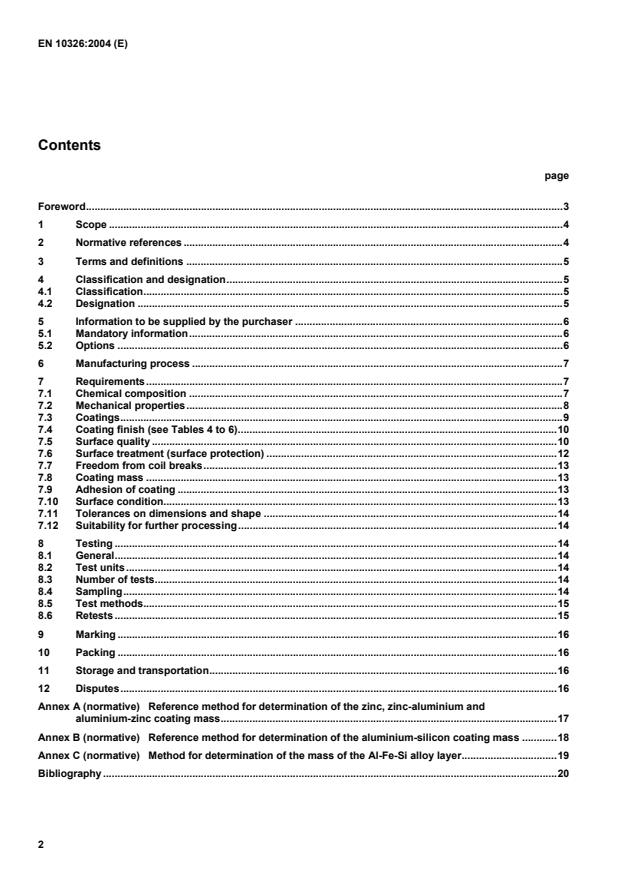
Reference method for determination of the zinc, zinc-aluminium and aluminium-zinc coating mass.17 Annex B (normative)
Reference method for determination of the aluminium-silicon coating mass.18 Annex C (normative)
Method for determination of the mass of the Al-Fe-Si alloy layer.19 Bibliography.20
EN 10169-3); • continuously hot-dip coated strip and sheet of steels with higher yield strength for cold forming (see EN 10292). 2 Normative references The following referenced documents are indispensable for the application of this document. For dated references, only the edition cited applies. For undated references, the latest edition of the referenced document (including any amendments) applies. EN 10002-1, Metallic materials - Tensile testing - Part 1: Method of test at ambient temperature. EN 10020:2000, Definition and classification of grades of steel. EN 10021:1993, General technical delivery requirements for steel and steel products. EN 10027-1, Designation systems for steels - Part 1: Steel names, principal symbols. EN 10027-2, Designation systems for steels - Part 2: Numerical system. EN 10079:1992, Definition of steel products. EN 10143, Continuously hot-dip metal coated steel sheet and strip - Tolerances on dimensions and shape. EN 10204:1991, Metallic products - Types of inspection documents. CR 10260, Designation systems for steel - Additional symbols.
special tolerances; e) term "steel"; f) number of this document (EN 10326); g) steel name or steel number and symbol for the type of hot-dip coating as given in Table 1; h) number designating the nominal mass of coating (e.g. 275 = 275 g/m² including both surfaces, see
Tables 3 to 6); i) letter denoting the coating finish (N, M or R, see 7.4 and Tables 4 and 5); j) letter denoting the surface quality (A, B or C, see 7.5 and Tables 4 to 6); k) letter denoting the surface treatment (C, O, CO and S, see 7.6). EXAMPLE 1 sheet, delivered with dimensional tolerances in accordance with EN 10143 with nominal thickness of 0,80 mm, ordered with special thickness tolerances (S), nominal width 1 200 mm, ordered with special width tolerances (S), nominal length 2 500 mm, ordered with special flatness tolerances (FS), made of steel S320GD+Z (1.0250+Z) in accordance with EN 10326, coating mass 275 g/m² (275), coating finish M, surface quality B, chemically passivated (C):
1 sheet EN 10143-0,80Sx1200Sx2500FS
steel EN 10326-S320GD+Z275-M-B-C or:
1 sheet EN 10143-0,80Sx1200Sx2500FS
steel EN 10326-1.0250+Z275-M-B-C 5.2 Options A number of options are specified in this document and listed below. lf the purchaser does not indicate his wish to implement one of these options, the products shall be supplied in accordance with the basis specification
(see 5.1). a) delivery of products in thicknesses > 3 mm (see 1.2); b) verification of the product analysis (see 7.1.2);
Table 1 — Steel grades and mechanical properties (longitudinal test pieces) Designation Chemical composition % by mass max. Mechanical properties Steel grade Steel name Steel number Symbols for the types of hot-dip coating C Si Mn P S 0,2 %-proof strength Rp0,2 a MPa * min. Tensile strength Rm b MPa * min. Elongation A80 c % min. S220GD 1.0241 +Z,+ZF,+ZA,+AZ 220 300 20 S250GD 1.0242 +Z,+ZF,+ZA,+AZ,+AS 250 330 19 S280GD 1.0244 +Z,+ZF,+ZA,+AZ,+AS 280 360 18 S320GD 1.0250 +Z,+ZF,+ZA,+AZ,+AS 320 390 17 S350GD 1.0529 +Z,+ZF,+ZA,+AZ,+AS 350 420 16 S550GD 1.0531 +Z,+ZF,+ZA,+AZ
0,20
0,60
1,70
0,10
0,045550 560 - * 1MPa = 1 N/mm2. a If the yield point is pronounced, the values apply to the upper yield point (ReH). b For all grades except S550GD, a range of 140 MPa can be expected for tensile strength. c For product thicknesses ≤ 0,70 mm (including coating) the minimum elongation values (A80) shall be reduced by 2 units.
Table 2 — Permissible deviations of the product analysis from specified limits on cast analysis given in Table 1 Element Specified limit of the cast analysis in Table 1 % by mass Permissible deviation of the product analysis % by mass C 0,20 + 0,02 Si 0,60 + 0,03 Mn 1,70 + 0,10 P 0,10 + 0,01 S 0,045 + 0,005
7.2 Mechanical properties 7.2.1 The products shall be supplied on the basis of the mechanical property requirements in Table 1. 7.2.2 lf so agreed at the time of enquiry and order, products specified in Table 1 may be supplied with suitability for manufacturing a specific part. In this case the values given in Table 1 do not apply. The reject tolerances arising when the material is processed shall not exceed a specific proportion to be agreed at the time of enquiry and order. 7.2.3 A reduction in the formability of all the coated products specified in this standard may occur by ageing. Therefore it is in the interest of the user to use the products as soon as possible after receiving them. 7.2.4 The tensile test values apply to longitudinal test pieces and are related to the test piece cross section without coating.
...